Lightweight Hygienic Cable Carriers for Food Processing
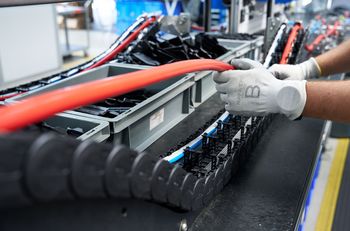
In food and beverage manufacturing, hygiene, safety, and efficiency are equally important. Cable management systems must not only protect moving cables but also meet strict sanitation requirements. This is why a lightweight hygienic cable carrier has become a preferred solution for modern food processing equipment. Designed for cleanliness and reliability, these systems help manufacturers maintain compliance while improving operational performance.
Unlike traditional industrial cable carriers, hygienic designs focus on smooth surfaces, minimal gaps, and materials suitable for washdown environments. Combined with reduced weight and optimized structure, they deliver superior performance in high-speed, high-cycle production lines.
Why Lightweight Design Matters in Hygienic Environments
A lightweight energy chain system reduces mechanical load on moving parts, making it ideal for fast-paced food processing equipment such as conveyors, packaging machines, and sorting systems. Lower mass means less inertia, smoother motion, and reduced wear on both cables and machinery.
Lightweight systems also simplify installation and maintenance. Operators can quickly access cables without heavy tools, reducing downtime during cleaning or reconfiguration. For food manufacturers focused on efficiency, lightweight construction directly supports higher uptime and lower operational costs.

Easy Clean Cable Management System for Food Safety
An easy clean cable management system is essential in environments where daily washdowns and strict hygiene protocols are required. Hygienic cable carriers are engineered with open or self-draining designs that prevent water, food residue, and bacteria from accumulating.
Key features often include:
-
Rounded edges to eliminate dirt traps
-
Smooth, non-porous materials resistant to chemicals
-
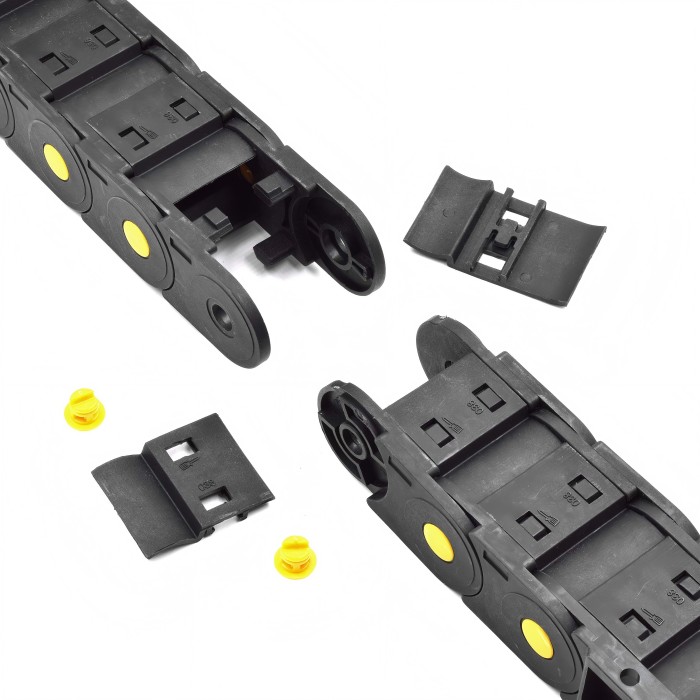
Tool-free opening for fast inspection and cleaning
-
Compatibility with CIP (Clean-in-Place) procedures
These features make easy-clean systems a reliable choice for food-grade automation.
Food Processing Cable Carrier Applications
A specialized food processing cable carrier is widely used in meat processing lines, dairy production, beverage bottling, bakery equipment, and frozen food handling systems. In these environments, cable carriers must withstand moisture, temperature changes, and frequent sanitation without degrading.
Lightweight hygienic cable carriers support power cables, sensor lines, and pneumatic hoses while maintaining stable motion and high cleanliness standards. Their modular design allows easy customization for different machine layouts and travel lengths.

Choosing the Right Hygienic Energy Chain Solution
When selecting a lightweight energy chain system, food manufacturers should consider material certification, cleanability, and long-term durability. Working with experienced suppliers ensures compliance with food safety standards while delivering reliable cable protection.
By investing in a lightweight hygienic cable carrier, food processing facilities can achieve cleaner production, safer operations, and more efficient automation—without compromising on performance or hygiene.


Drag Chain Thingiverse Designs vs Industrial Cable Chains
Bearing Cable Drag Chains for Heavy Gantry Systems